Two product markets. One integrated approach.
Specify your end product first. We then align the feedstock route, separation system, utilities and plant interfaces around the required quality and capacity.
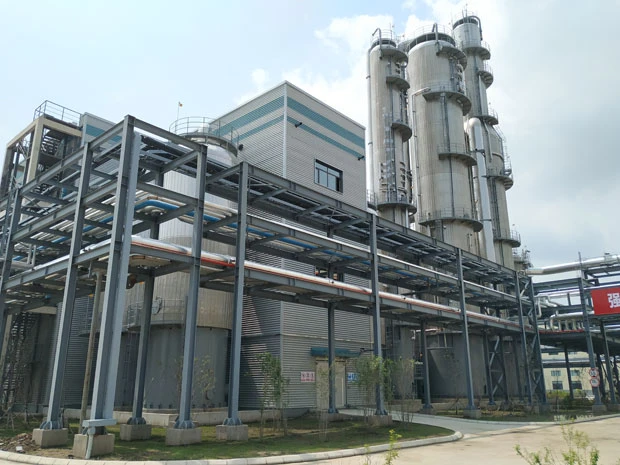
Fuel ethanol plants
Integrated ethanol production systems for fuel markets, with fermentation, heat-integrated distillation and molecular-sieve dehydration engineered as a coordinated process.
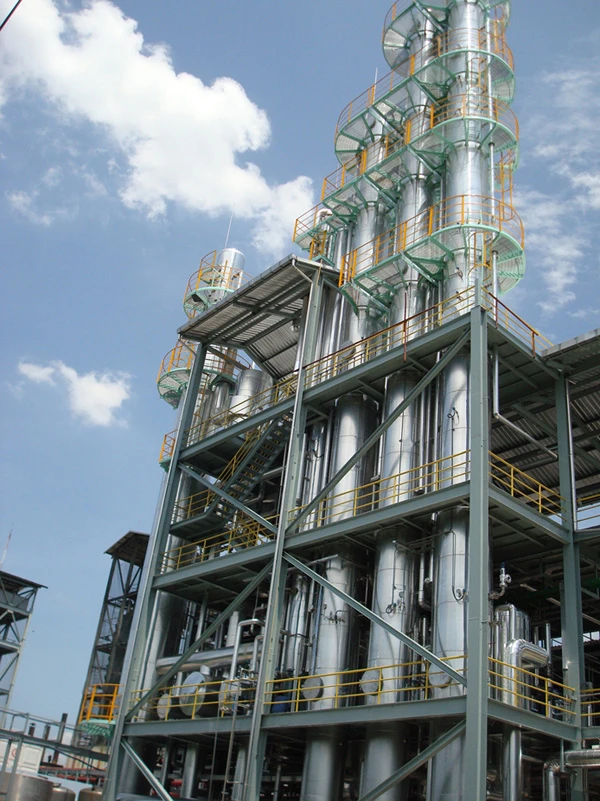
Food-grade ethanol & ENA ethanol plants
Precision separation for neutral alcohol applications. The process is selected around impurity control, sensory quality and the buyer’s complete product specification.
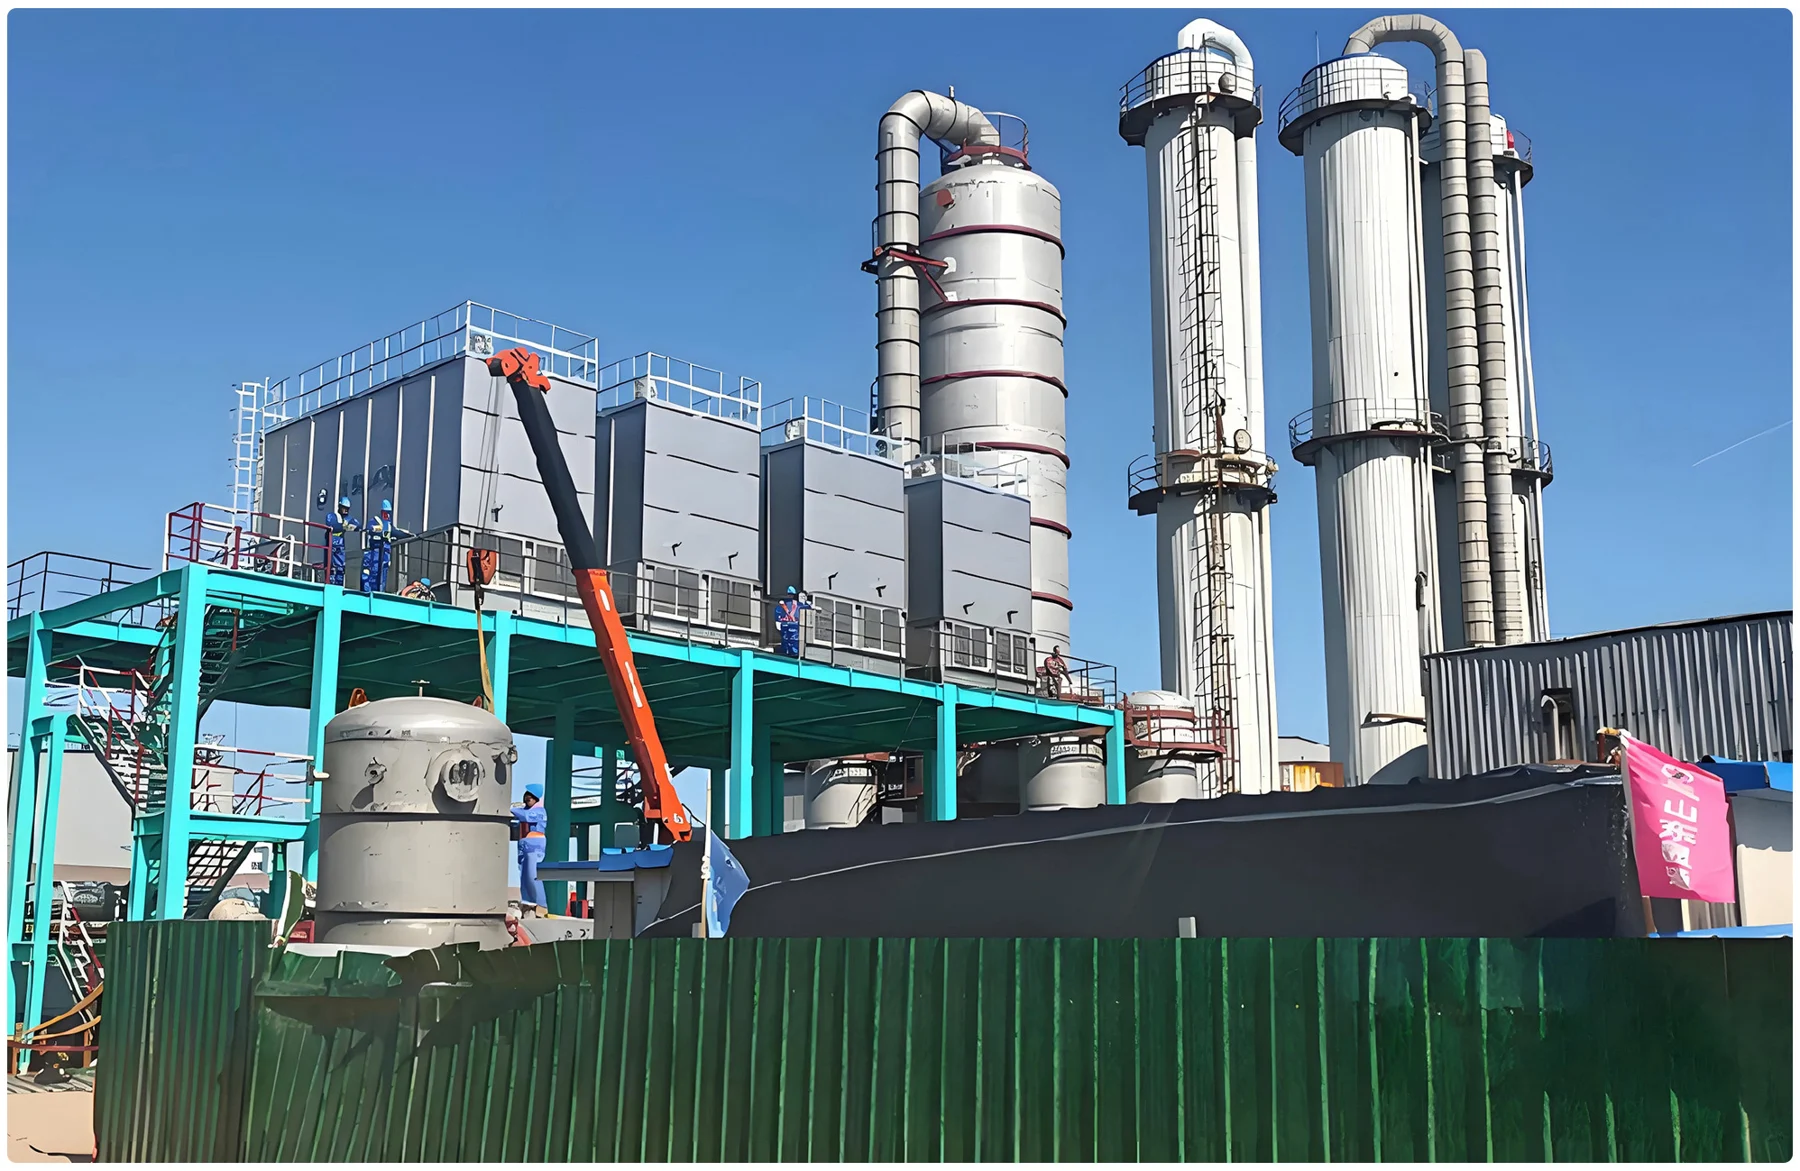
Xanthan-gum alcohol recovery
Return alcohol to the xanthan-gum process at the required reuse quality. Variable solvent strength, entrained solids, fouling and residue handling shape the recovery train. Our Meihua and Zhongxuan projects include alcohol recovery and modifications to existing distillation systems.
Explore the engineering behind the project
CNE / Discuss your project
Your next plant starts with the right conversation.
Share your feedstock, target product and capacity. Let’s shape a practical process concept.