Feed preparation, liquefaction & fermentation
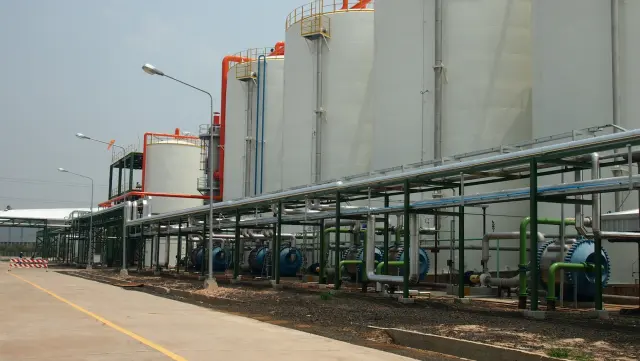
The front end sets the conditions for downstream separation. Our cassava front end integrates storage, milling, liquefaction, saccharification and controlled fermentation.
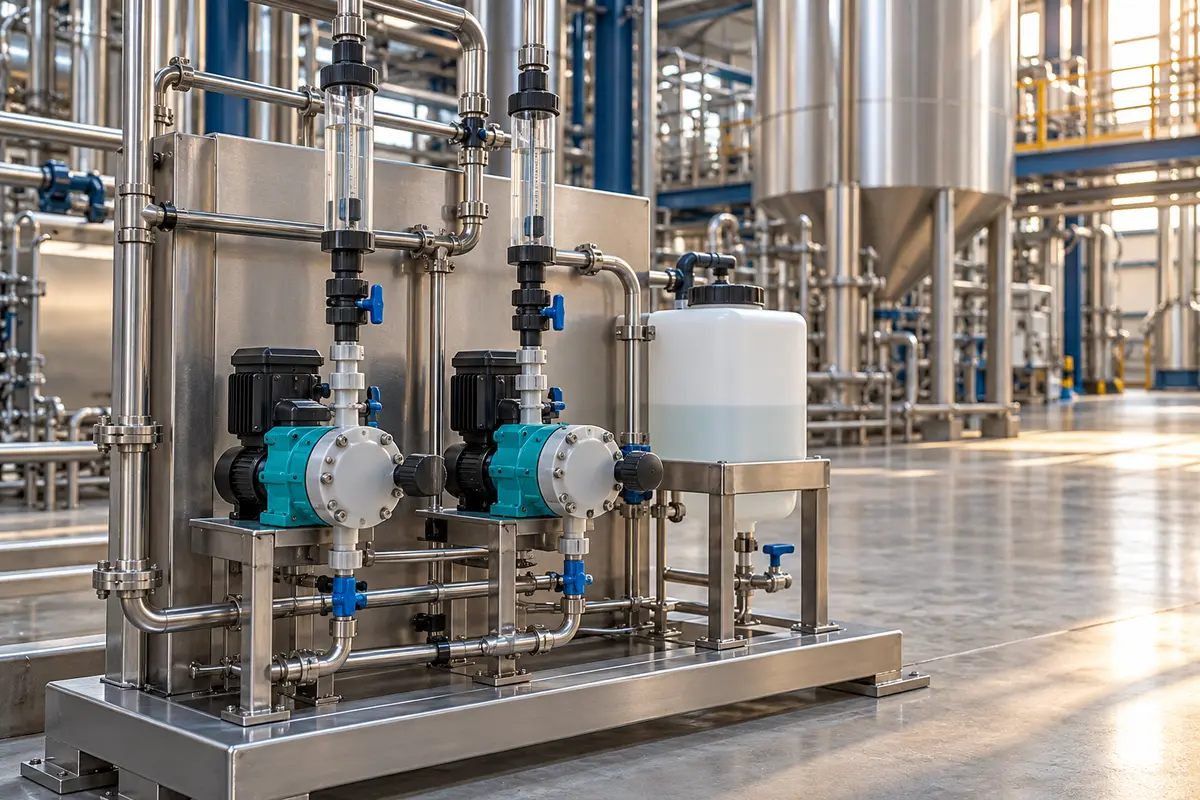
Explore ↗A dosing-pump setting is not a measured enzyme consumption. Reconcile the delivered dose, feed mass and enzyme specification before drawing conclusions about conversion or cost.
CNE — China New Energy · Updated ·
AI · Process illustration — not a site photograph
01 /
State whether the dose is expressed per tonne of wet feed, dry feed or starch, and whether the quantity refers to commercial liquid or active enzyme units. Record feed moisture and starch basis beside the calculation. Two suppliers can specify different activity concentrations; comparing their kilograms alone can give a misleading result.
02 /
Use a calibrated mass measurement or a vessel-volume change over a defined period, with the density needed for a volume-to-mass conversion. Account for refill events, dilution, returns and any shared dosing lines. Compare the measured delivery with the feed throughput over the same time window. A pump stroke or speed setting needs a verified calibration curve under its installed conditions.
Dose in kg/t = enzyme mass delivered in kg / feed mass processed in tonnes. For example, 12 kg delivered while processing 40 tonnes corresponds to 0.30 kg/t. This is a calculation example, not a recommended process dose.
03 /
Check pump condition, priming, trapped gas and line restrictions when indicated delivery disagrees with measured usage. Compare conversion and fermentation data using the same sampling times and methods. A laboratory trend is meaningful only when temperature correction, sample preparation and reporting units are consistent. Changes to enzyme selection or dose should follow the supplier’s specification and the site’s approved process-change procedure.
04 /
Use one approved dosing sheet across operations and the laboratory. Train operators to record tank refills, pump settings, measured delivery and raw-material throughput. A shared calculation basis makes enzyme consumption and conversion results easier to compare.
05 /
Record enzyme product and batch, declared activity, storage conditions, feed mass and moisture, measured delivery, calibration date, dosing location and the corresponding conversion results. Keep changes in a dated log so a consumption reduction can be assessed together with product yield and fermentation stability.
Updated · 2026-10-11
The front end sets the conditions for downstream separation. Our cassava front end integrates storage, milling, liquefaction, saccharification and controlled fermentation.
Explore ↗
An alcohol specification combines concentration, impurity limits and agreed test methods. Our laboratory approach covers both process checks and finished-product analysis.
Explore ↗Define the control narrative, instrument list, I/O, alarms and interlocks together with the process design. PLC or DCS architecture, hazardous-area suitability, remote support and site integration are agreed for the project.
Explore ↗From cassava to corn: CNE integrates process design, new and existing equipment, and on-site commissioning support for PT Indonesia Ethanol Industry.
Explore ↗Share your feedstock, target product and capacity. Let’s shape a practical process concept.
